Description
A custom boring tool with internal coolant and three-point clamping should be reviewed as a complete machining assembly. Bore diameter alone is not enough: the bore geometry, machining stage, machine interface, tool overhang, coolant route, clamping datum and inspection method all influence the final design.
What should be confirmed before a custom boring tool is reviewed?
- Workpiece drawing, material, hardness or material condition when known
- Bore diameter, depth, tolerance, surface requirement and any step or chamfer
- Roughing, semi-finishing or finishing operation and the available stock allowance
- Through bore, blind bore, interrupted section and required chip-evacuation direction
- Machine-side interface, rotation direction, available overhang and collision limits
- Coolant type, connection and available pressure or flow data when known
- Three-point clamping or locating dimensions, datum surfaces and actuation method
- Required runout, inspection datum, quantity and drawing revision
Bore geometry and process sequence
In practice, a through bore and a blind stepped bore place different demands on tool clearance and chip exit. State whether the tool must bore, chamfer, back-bore or machine several features in one setup. The pre-bore condition and stock distribution should also be included, because an uneven allowance can change the cutting load.
If several cutting features are requested on one body, identify the machining order and the acceptance requirement for each feature. This helps separate necessary functions from dimensions that can remain adjustable or replaceable.
Internal coolant, clamping and machine interface
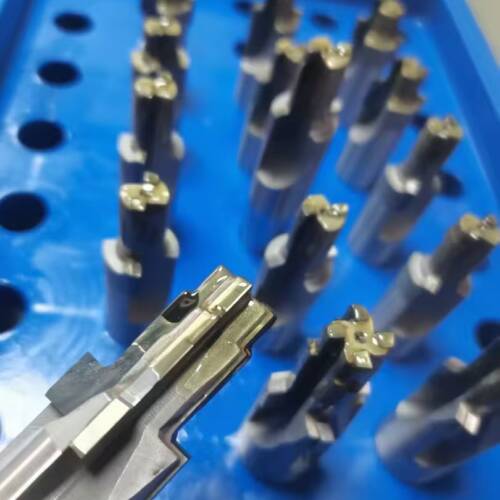
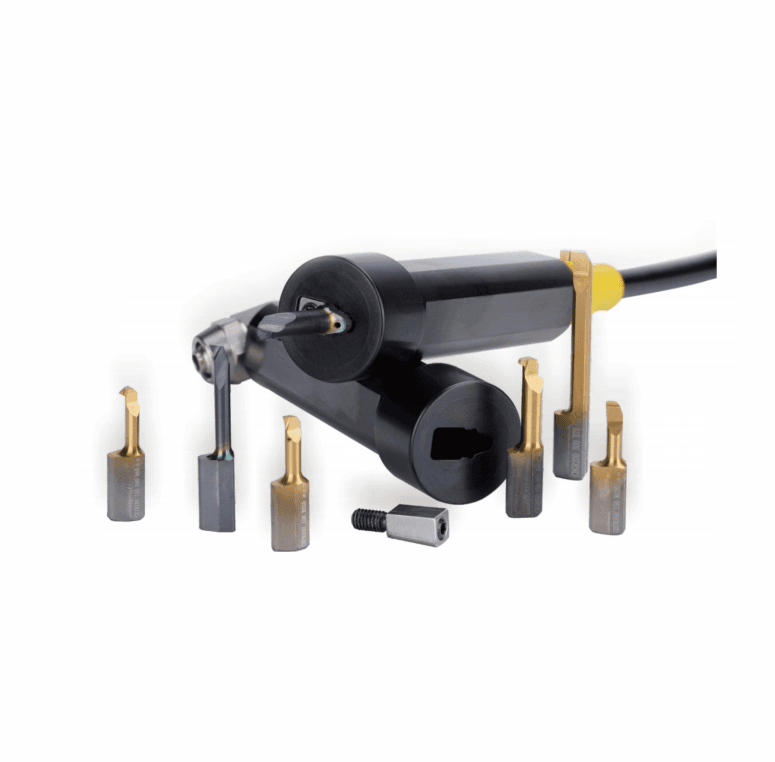
Internal coolant routing should be matched to the machine connection, available coolant supply, cutting-edge position and chip path. A coolant port shown in a photograph does not establish pressure, flow or compatibility; those details should come from the machine and tool-interface data.
The three-point clamping or positioning arrangement is project-specific. Send the mating dimensions, locating faces, tightening or actuation method and permitted access space. Inspection should reference an agreed datum and assembly condition rather than an isolated tolerance value.
Questions buyers usually ask
Can one custom boring tool machine several bore features?
It may be possible to combine boring, step, chamfer or back-boring features, but the decision depends on the feature sequence, available space, adjustment method, chip clearance and inspection plan.
What coolant information should I provide?
Provide the coolant type, machine connection, available pressure and flow when known, and whether the bore is through, blind or interrupted. Also identify any chip-evacuation problem in the current process.
What information is needed for an RFQ?
Send the workpiece drawing, bore features and tolerances, material condition, machine and interface data, operation sequence, current tool or setup, coolant information, quantity and inspection requirements.
Request a custom boring-tool review
Use the Full RFQ form to upload the workpiece and interface drawings. For other drawing-based tooling, see Custom Tools.
Quick Product Inquiry
Ask about tooling, lead time, or application fit. We will reply with a tailored recommendation.
Need to upload drawings or full machining data? Use Full RFQ